
Safety
Repairs on heavy plant need to be controlled. Cracks are tested and prepared before they are welded, and every job follows the rules of the site it is on.
Repair controls
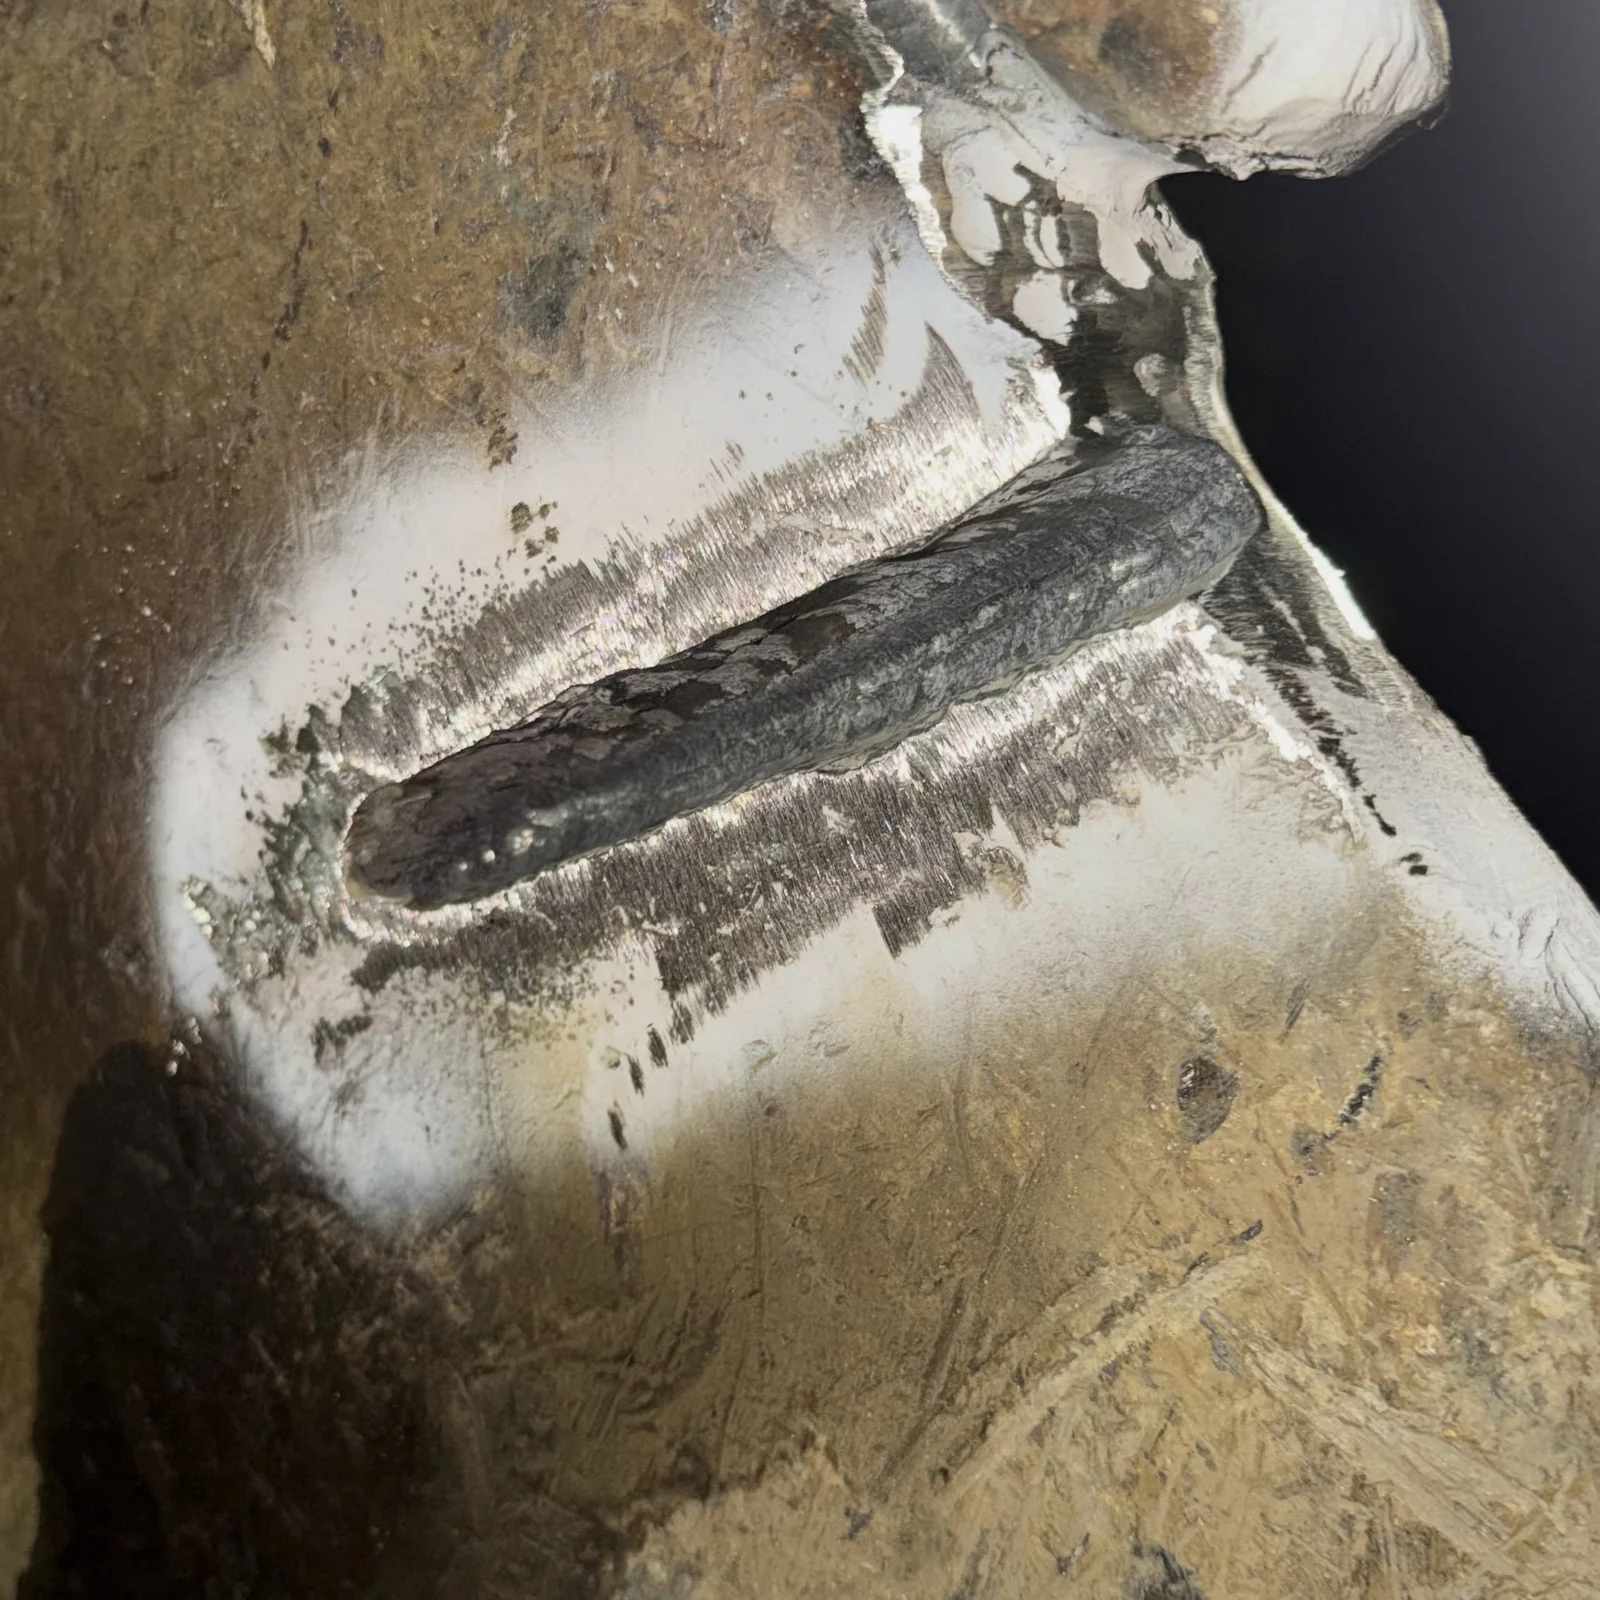
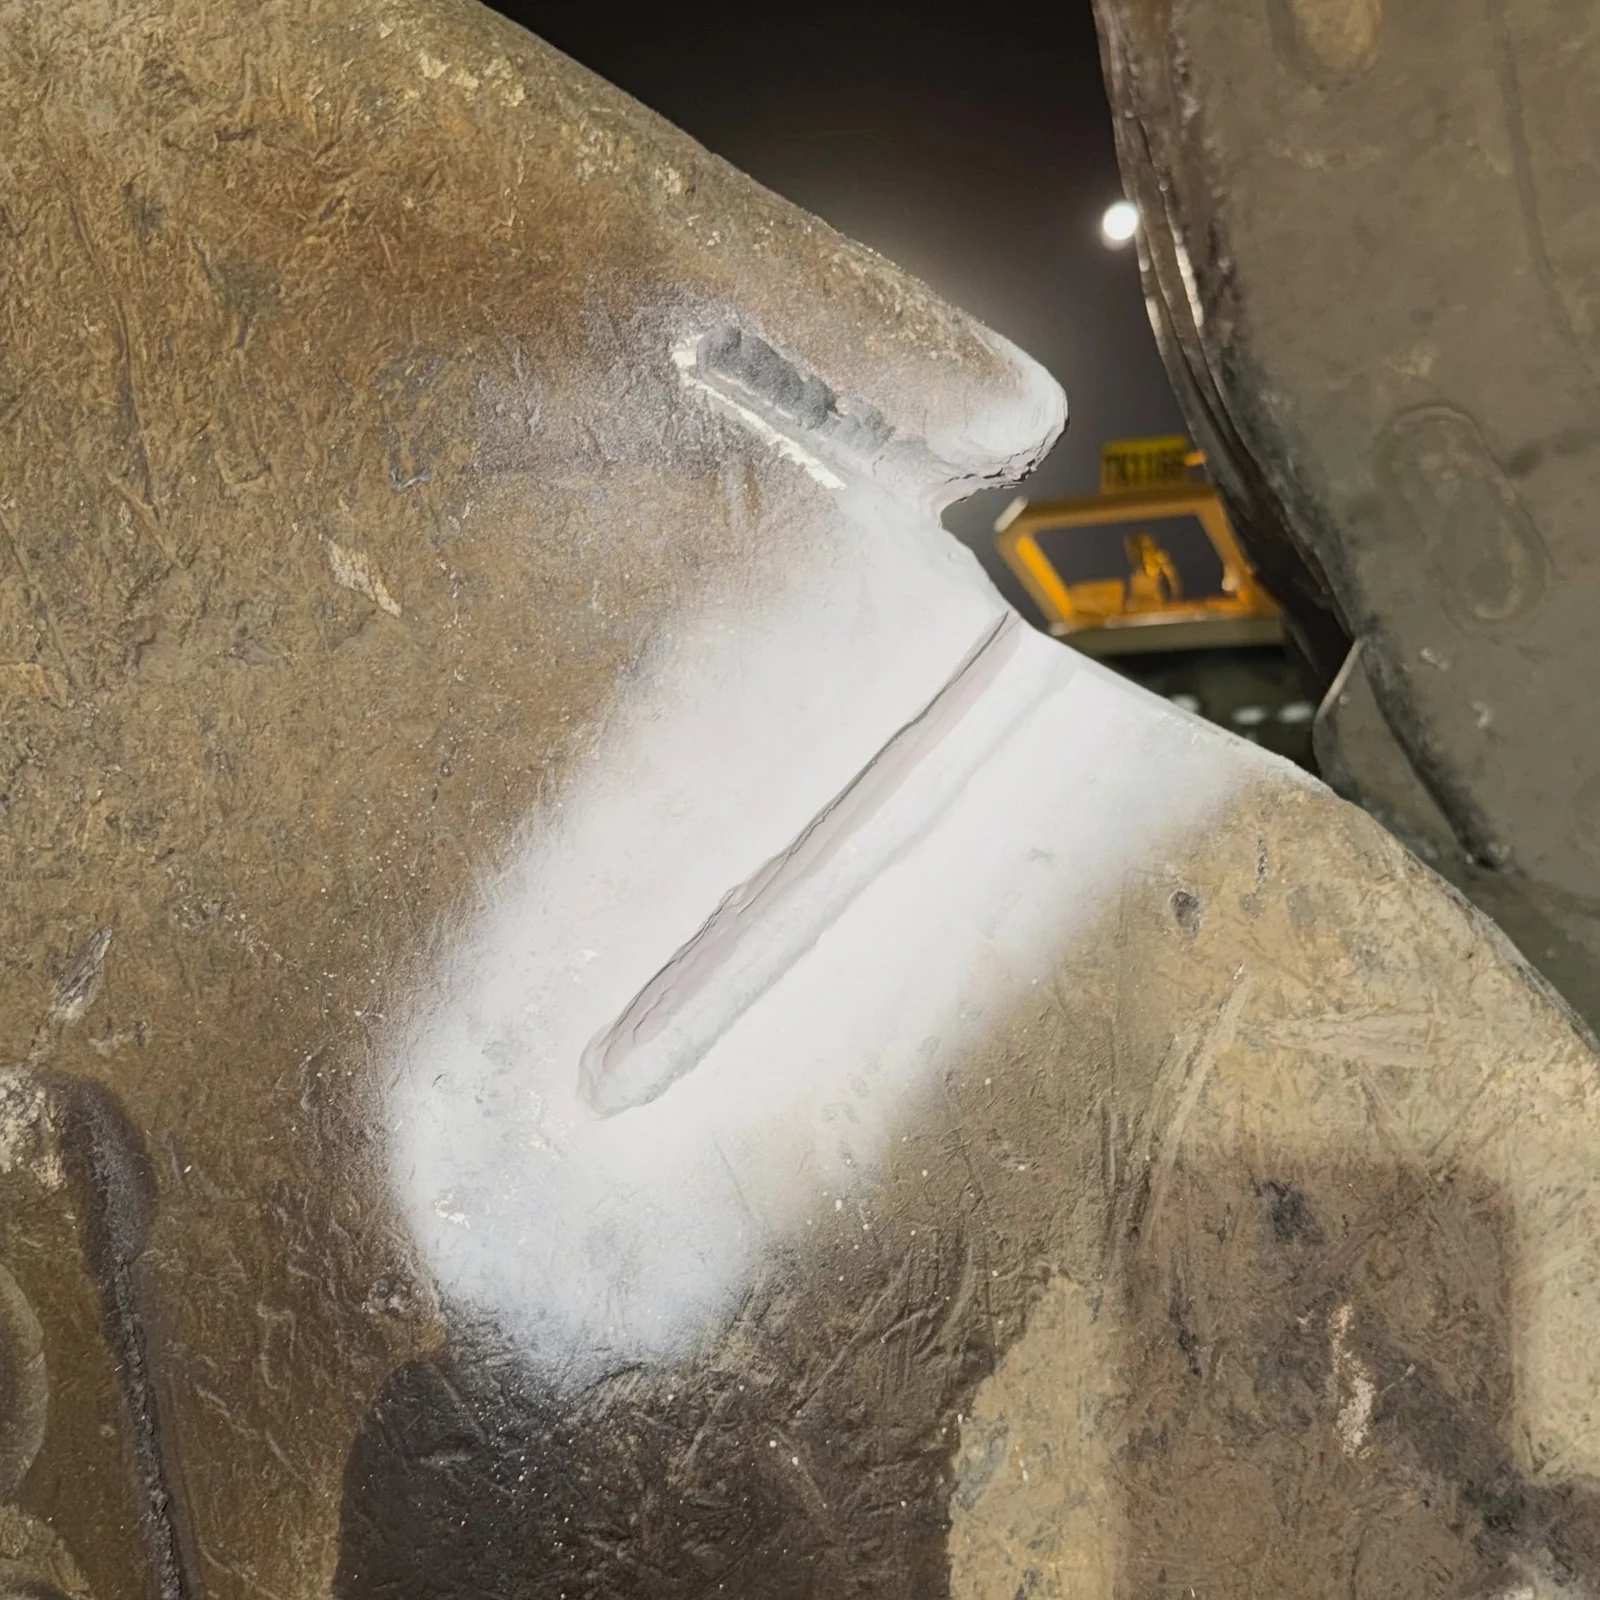
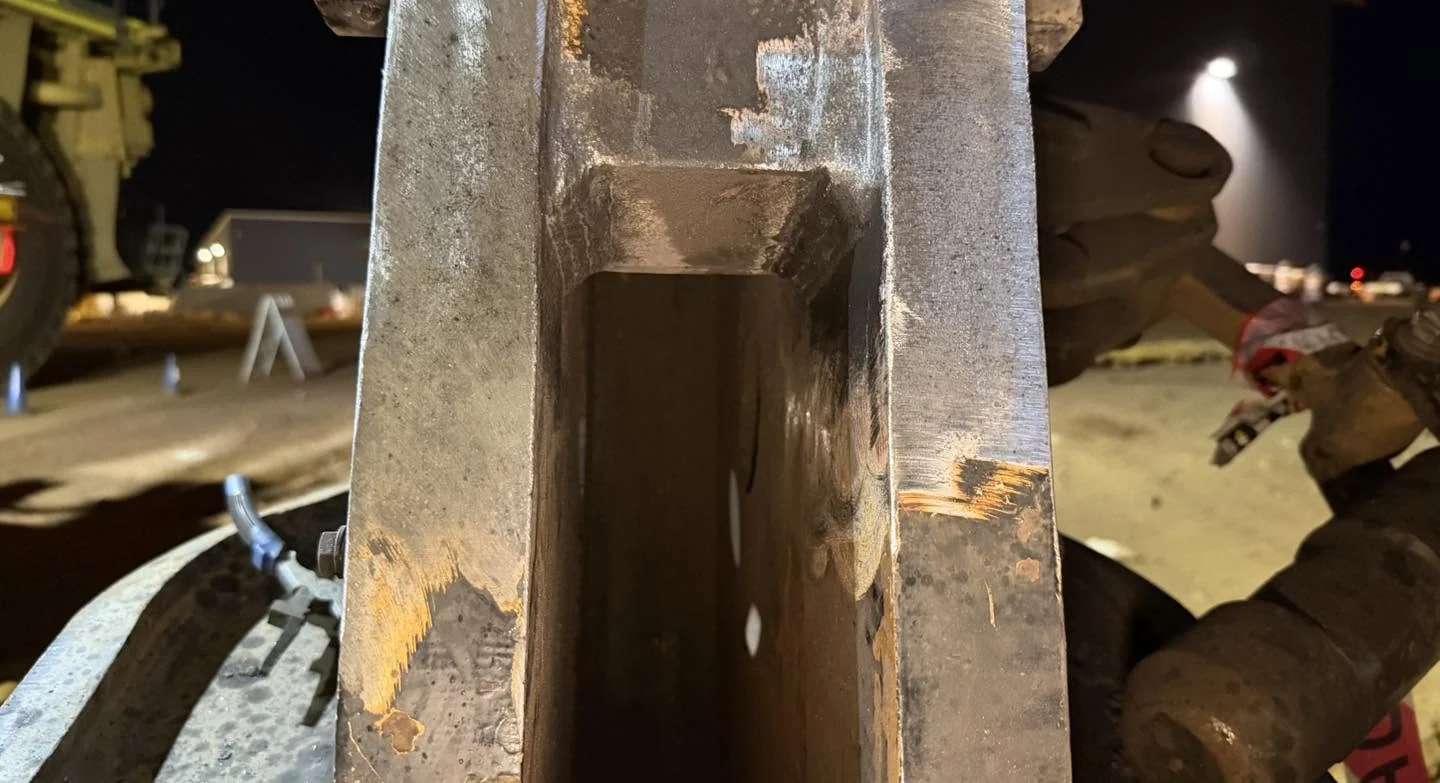
From the Liebherr 9400 side wall crack repair. The same discipline applies to every crack repair.
Crack tested and identified
Cracks are located by magnetic particle inspection (MPI) so the full extent is known before repair.
Gouged out and checked
The crack is gouged out and the groove checked for impurities before any weld is laid.
Weld procedure followed
The weld repair procedure is followed and executed to complete the repair.
Working on your site
Site managers need to know who is coming onto site and how the work is controlled. This is what to expect from an Oreweld job.
Site inductions
We complete the inductions each site requires before work starts.
Tickets and licences
Work is done by qualified tradespeople holding the tickets each site asks for.
Permits and isolation
Machines are isolated and site permits followed before any welding begins.
A controlled work area
Hot work areas are set up and checked, and left clean when the job is done.
Tell us what needs repairing
Send what needs repairing, where the machine is located and a few photos of the job. We will discuss the best way to help.